cobalt
M42
It offers high mechanical wear resistance due to the optimally heat-treated microstructure of the tooth tip.
cobalt
forte C
Such as bi-alfa®cobalt M42 with a special forteC coating to enhance cutting performance and thermal resistance.
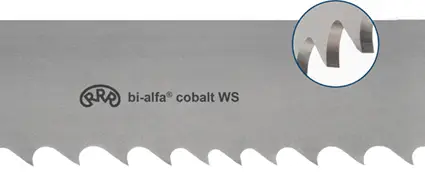
cobalt WS
Greater cutting width thanks to HSS-M42 tooth tips. This creates a wider cutting channel.

cobalt WS
ALU
Features an additional rake angle and an aggressive chip angle. Better chip formation and good clearance.
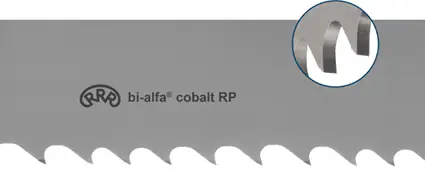
cobalt
RP
The rake angle at the tip of the tooth is 16°, which gives the band aggressive cutting performance.
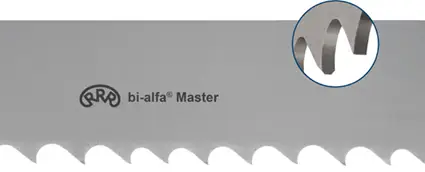
Master
Improved cutting performance thanks to the borazon-ground bevel on the saw band's lead-in tooth (A).
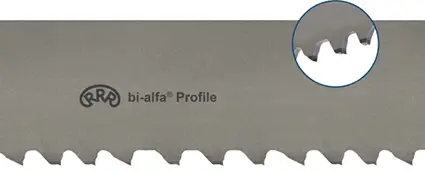
Profile
Bi-alfa Profile is the saw blade that delivers the best cutting results for round and square tubes and profiles.
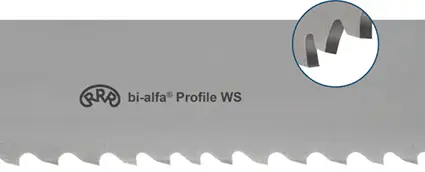
Profiles WS
The Profile WS series ensures a perfect cut for sawing tasks prone to vibration.
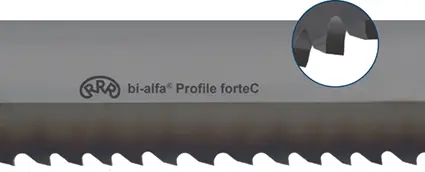
Profile
forte C
Also available with a special forteC coating to improve cutting performance and thermal resistance.
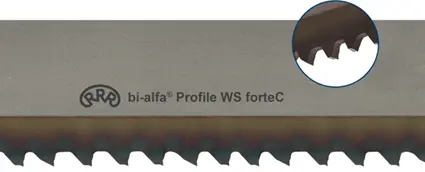
Profile
WS forteC
Also available as bi-alfa® Profile WS with a special forteC coating to enhance cutting performance and thermal resistance.
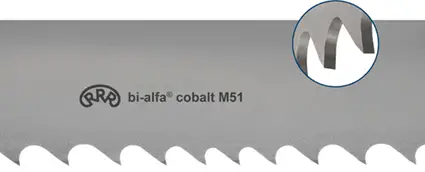
cobalt
M51
Featuring a base strip made of high-alloy tempered steel and HSS-M51 for the tooth tips.
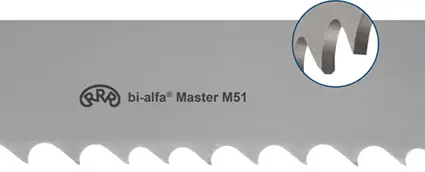
Master
M51
Tooth tips made of HSS-M51 with very tight tooth height tolerances. Each tooth is subjected to uniform stress.
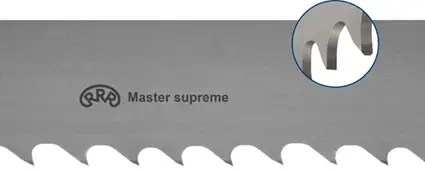
Master
supreme
Machining of all common steel grades up to a hardness of 50 HRC. Extra-wide chamfer for materials with residual stress.
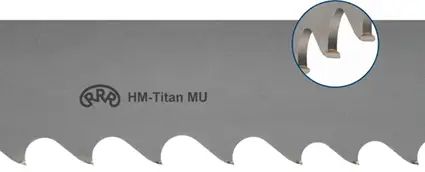
MU
Versatile application; machining of all common steel grades up to a hardness of 1700 N/mm².
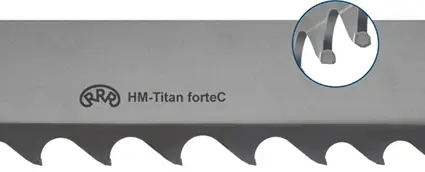
forteC
It consists of a specially alloyed tempered steel carrier strip and tooth tips made of high-quality carbide.
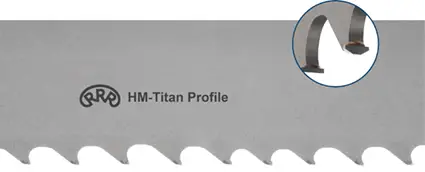
Profile
Features a robust VN geometry and is suitable for machining all common types of steel.
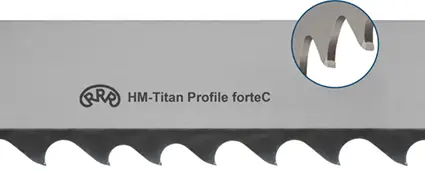
Profile
forte C
Robust cutting edge geometry for machining all common steel grades up to a hardness of 1900 N/mm².
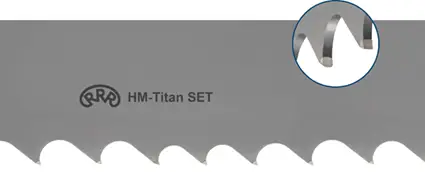
SET
A band saw blade is particularly suitable for cutting materials with internal stresses.
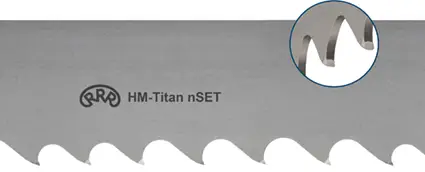
nSET
High-performance band saw blade for cutting all common types of steel with a tensile strength of up to 1700 N/mm².
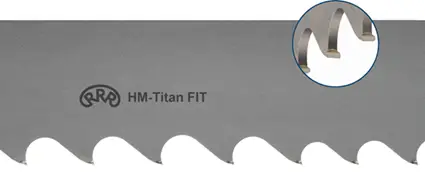
FIT
High-wear-resistant carbide body, high-performance band saw blade specifically designed for cutting nickel-based alloys.
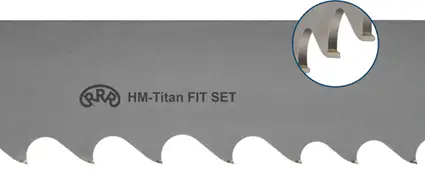
FIT
SET
High-performance band saw blade with Multispan geometry, specially designed for cutting nickel-based alloys.
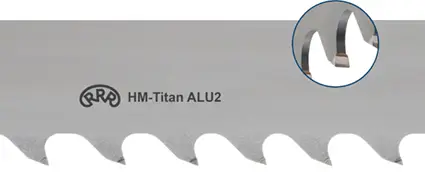
ALU2
Optimized for sawing non-ferrous metals, particularly aluminum, and suitable for all standard workpieces made of these materials.

ALU3
Optimized for sawing non-ferrous metals, particularly aluminum. Suitable for sawing blocks and sheets.
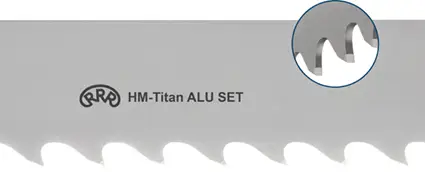
ALU SET
Specifically designed for cutting non-ferrous metals, particularly aluminum.
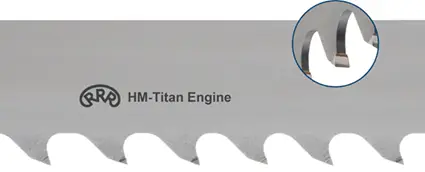
Engine
Specially designed for abrasive, high-silicon alloys and for use with graphite.
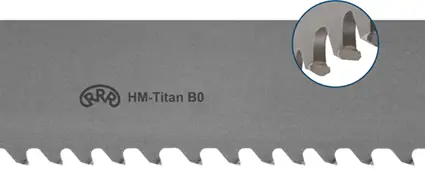
B0
Designed for sawing hardened or induction-hardened materials with a hardness of >50 HRc.
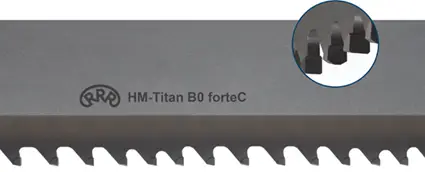
B0
forte C
For machining hardened, induction-hardened, and ultra-hard materials with a hardness of over 50 HRC.
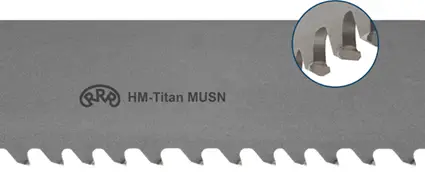
MUSN
Recommended for use on high-performance sawing machines and for cutting high-hardness workpieces.
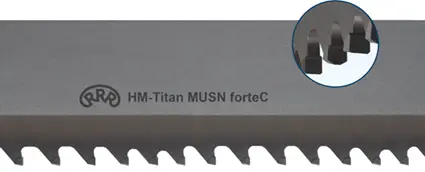
MUSN
forte C
Machining of hardened/induction-hardened and ultra-hard materials > 50 HRC.
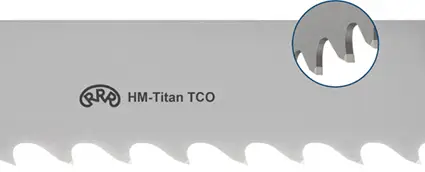
TCO
Low cutting pressure, resulting in less tiring work when feed is primarily manual.
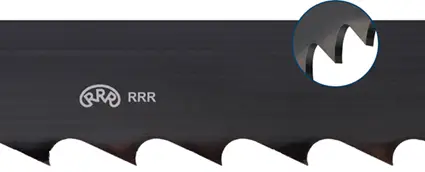
RRR
Manufactured from strip steel with a pinpoint microstructure (carbide density of 30–50 carbide grains per µm²).
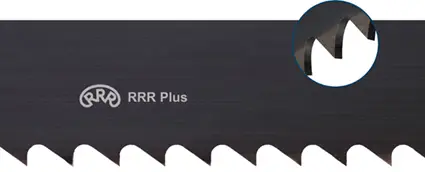
RRR
Plus
Manufactured from strip steel with a pinpoint microstructure (carbide density of 30–50 carbide grains per 100 µm²).
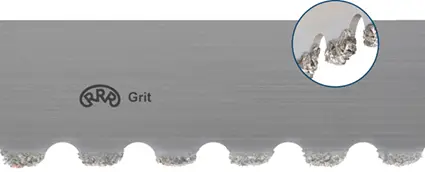
Segmented
Contains a large number of polygonal carbide grains permanently bonded to a highly flexible backing tape.
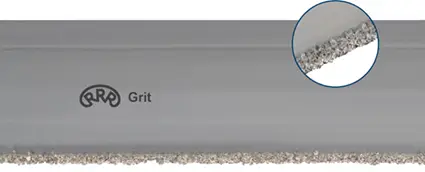
Continuously
Contains a large number of polygonal carbide grains permanently bonded to a highly flexible backing tape. Continuously distributed.
Machine-
-sawing
Our high-performance machine saw blades are ideal for everything from plain carbon steel to chromium-nickel steel.
hand hacksaw
blades
Made from the finest high-speed steel or as a bimetal saw blade: our solution for the most demanding applications.